China Top Cable Harness Manufacturers for Global Buyers

China has become a major sourcing destination for reliable cable harness production. Its manufacturers serve automotive, industrial, medical, energy, and consumer electronics markets. However, choosing a suitable partner requires more than comparing factory prices.

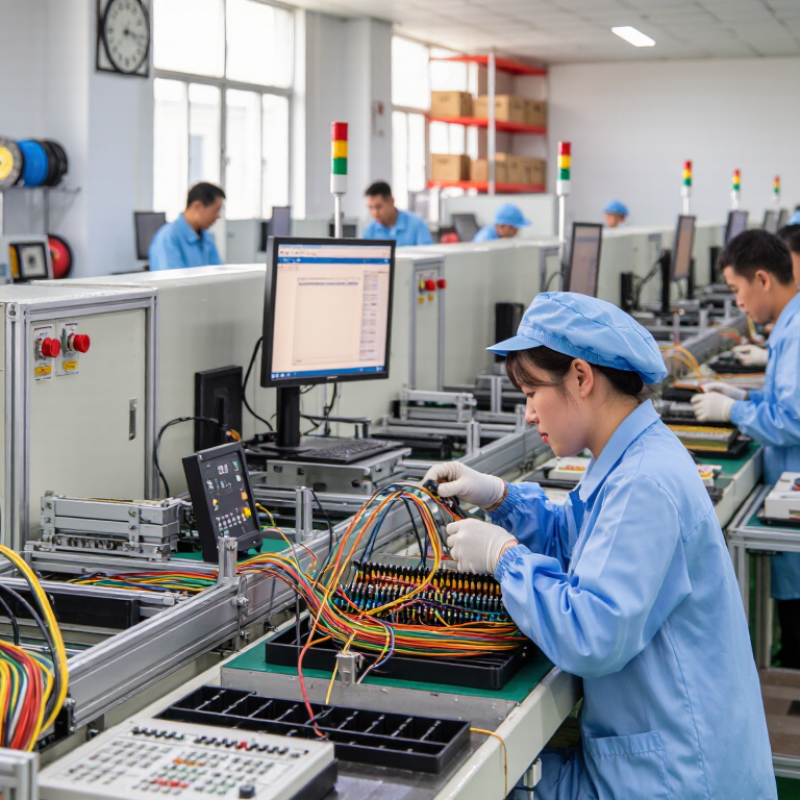
Experienced buyers examine engineering depth, production controls, and communication habits. A dependable supplier should interpret drawings accurately and question unclear specifications. It should also manage wire cutting, terminal crimping, labeling, bundling, and final inspection with consistency. Small details matter. A loose terminal can stop an entire machine.

This guide explores China’s top cable harness manufacturers for global buyers. It focuses on capabilities, certifications, testing methods, industries served, and export experience. Practical evaluation points include sample approval, bill-of-material control, traceability, and packaging quality. Buyers should request evidence rather than accept attractive claims. For example, ask for crimp-force records, continuity-test reports, and clear photos of production lines. A factory visit can reveal more than a polished website.

No supplier is perfect. Even a strong manufacturer may struggle with urgent engineering changes or low-volume orders. Buyers should discuss these weaknesses early. Honest answers often indicate stronger cooperation later. Certification also needs careful checking. An ISO certificate alone does not prove every harness meets your application requirements. Product-specific testing remains essential.

The best partnership balances technical skill, stable quality, transparent pricing, and responsive service. This overview helps purchasing teams compare manufacturers with greater confidence. It also encourages careful verification before production begins. Reliable sourcing starts with questions, not assumptions.

China Top Cable Harness Manufacturers for Global Buyers

Cable Harness Market Scope: Applications, Materials, and 10 RoHS-Restricted Substances

For global buyers, the cable harness market spans vehicles, industrial controls, medical equipment, appliances, and communication devices. Each application demands different current ratings, bend performance, and temperature resistance. Copper conductors support efficient transmission, while insulation may use PVC, silicone, TPU, or polyethylene. A flexible door harness needs different construction from a fixed control-panel assembly. Small details matter.

RoHS requirements under European rules restrict ten substances:

lead, mercury, cadmium, hexavalent chromium, PBB, PBDE, DEHP, BBP, DBP, and DIBP.

These substances may appear in solder, pigments, cable insulation, plating, or plasticizers. A capable manufacturer should provide material declarations, production records, and traceability for each batch.

XRF screening can identify several metals quickly, but it cannot confirm every restricted substance. Laboratory testing may still be necessary.

I have learned that a certificate alone can be insufficient. Buyers should compare test dates, sample descriptions, laboratory qualifications, and product versions.

Ask whether terminals, tapes, connectors, and overmolds were tested separately. This step is often missed. A material change can quietly alter compliance.

Application-specific exemptions may also affect evaluation, so technical teams should check the current market requirements before approval.

Keep records linked to cable length, lot number, and revision level.

How to Evaluate China Manufacturers Using IPC/WHMA-A-620 Class 2 and 3

China remains a major sourcing base as the global wire harness market expands. Fortune Business Insights valued this market at about USD 87.69 billion in 2023. Large capacity alone proves little. Buyers should evaluate each factory against IPC/WHMA-A-620, not marketing claims.

Class 2 suits general electronic products where continued performance matters. Class 3 demands tighter control for critical equipment and restricted failure tolerance. It is not simply “more testing.” Ask for controlled drawings, conductor preparation records, crimp-height data, and calibrated pull-force equipment. Inspectors should verify terminal position, exposed strands, insulation support, cavity locks, and identification marks. Request photographs of cross-sections. Then compare them with the approved workmanship criteria.

A capable Chinese manufacturer should separate Class 2 and Class 3 work instructions. Traceability should connect each harness to an operator, lot, tooling set, and inspection result. Continuity and insulation-resistance tests are useful, but they cannot replace visual checks. A clean test report can still hide weak strain relief. That is the uncomfortable part.

The standard does not replace your product drawing. Customer-specific requirements must define wire types, connector families, labeling, test limits, and sampling plans. During an audit, ask operators to explain one defect response without reading a script. Their answer often reveals more than a certificate. Fortune Business Insights, Wire Harness Market Report, 2024; IPC/WHMA-A-620, Cable and Wire Harness Assemblies.

China Top Cable Harness Manufacturers for Global Buyers - How to Evaluate China Manufacturers Using IPC/WHMA-A-620 Class 2 and 3
Evaluation Dimension Suggested Weight Class 2 Evaluation Benchmark Class 3 Evaluation Benchmark Objective Evidence to Request Buyer Verification Method
A. Standard Governance and Product Definition
Applicable workmanship standard 10% The supplier demonstrates that cable and wire harness workmanship is controlled against the applicable requirements of IPC/WHMA-A-620 Class 2, where continued performance is important but uninterrupted service is not always essential. The supplier demonstrates that workmanship is controlled against IPC/WHMA-A-620 Class 3, where continued high performance is essential and equipment downtime or failure may be unacceptable. Controlled workmanship specification, revision history, operator training records, internal audit reports, and purchase-order flow-down documents. Compare the purchase order, drawings, inspection plan, and work instructions. Confirm that the selected product class is explicitly stated rather than assumed.
Drawing and revision control 8% Current drawings identify wire type, conductor size, strip length, terminal, connector, cavity, branch length, labeling, and test requirements. The same information is controlled with tighter release discipline, documented approval, and traceable change implementation before production. Sample released drawing, bill of materials, engineering-change notice, revision register, and first-article approval record. Select one recent revision change and trace it from customer approval through material issue, production, inspection, and shipment.
Class assignment and risk analysis 7% The supplier can explain why the assembly is suitable for Class 2 service and identifies critical electrical, mechanical, and environmental characteristics. The supplier documents the higher consequence of defects and identifies characteristics requiring enhanced controls, inspection, and traceability. Process FMEA, control plan, critical-characteristic list, application information, and customer-approved acceptance criteria. Verify that the class assignment is consistent with the end-use risk, operating environment, and customer specification.
B. Materials, Crimping, and Mechanical Workmanship
Material and component traceability 10% Wire, terminals, seals, connectors, sleeves, and labels are identified by approved part number and controlled lot or batch information where required. Traceability is maintained from incoming material through finished assembly, with clear segregation of nonconforming or substituted components. Approved-vendor list, incoming inspection records, certificates of conformity, lot labels, material issue records, and substitution-approval records. Trace one finished harness backward to material lots and verify that unauthorized substitutions cannot enter production.
Wire preparation and conductor condition 8% Strip length, conductor exposure, insulation condition, and strand integrity meet the approved drawing and applicable workmanship requirements. Critical strip dimensions are controlled with documented setup verification and increased inspection where exposed conductor or insulation damage could affect reliability. Strip-length specification, setup checklist, first-piece approval, inspection gauges, defect samples, and operator qualification records. Measure samples from setup, mid-run, and end-of-run production. Check for nicked, cut, missing, or spread conductor strands.
Crimp quality and process capability 15% Crimp height, crimp width where specified, bellmouth, conductor brush, insulation support, terminal position, and pull performance meet approved requirements. The same characteristics are controlled with stronger emphasis on validated tooling, setup lockout, periodic verification, and documented reaction plans for drift. Crimp-height records, pull-test results, cross-section analysis where required, applicator maintenance logs, tooling setup sheets, and capability studies. Witness a crimp setup, inspect cross-sections or approved samples, review pull-test frequency, and confirm calibration status of measuring equipment.
Terminal and connector assembly 10% Terminals are fully seated, locks are engaged, seals are correctly positioned, cavities match the drawing, and connector bodies are free from damage. Terminal position, secondary locks, seals, keying, cavity occupancy, and connector retention are subject to documented 100% or risk-based controls as specified. Connector loading checklist, cavity map, terminal-retention test records, visual standards, poka-yoke controls, and error-proofing verification. Compare physical assemblies with the cavity map. Perform retention or pull-out checks using the approved method and sample plan.
Routing, branching, and protection 8% Branch lengths, bend radius, tie or clip positions, protective sleeving, conduit, grommets, and breakout locations conform to the drawing. Routing controls also address vibration, abrasion, heat, fluid exposure, strain relief, and installation orientation where these factors affect continued service. Assembly board, form-board verification, dimensional inspection report, routing template, fixture-maintenance record, and environmental design requirements. Check a finished harness against the drawing at datum points and verify that protection is not loose, damaged, over-compressed, or incorrectly positioned.
C. Inspection, Testing, and Reliability Controls
Electrical testing 15% Continuity, short-circuit, miswire, and connector-to-cavity checks are performed according to the approved test program and wiring definition. Electrical test coverage is supported by controlled test fixtures, verified programs, locked test parameters, and documented reaction to failures. Test program revision, fixture verification, tester calibration, test logs, failure records, repair authorization, and final-test acceptance criteria. Review test coverage against the pinout. Observe a challenge test using known open, short, and miswire conditions where permitted.
Dimensional and visual inspection 7% Inspection confirms key dimensions, markings, connector condition, workmanship, and packaging against the drawing and approved visual standards. Critical-to-function dimensions and visual characteristics have defined sampling or 100% inspection requirements, with clear acceptance and rejection limits. Inspection plan, calibrated measuring tools, visual defect catalogue, inspection records, and nonconformance disposition records. Audit inspection records against actual samples and verify that rejected parts are physically segregated and dispositioned by authorized personnel.
Calibration and measurement system control 5% Measuring and test equipment used for acceptance decisions is identified, calibrated or verified at defined intervals, and protected from misuse. Critical measurement systems have documented suitability, repeatability controls, and stronger evidence that test results remain reliable over time. Calibration certificates, equipment register, out-of-tolerance procedure, gauge verification records, and measurement-system studies where applicable. Select instruments at the production line and confirm identification, due date, range, resolution, and linkage to recorded results.
Process validation and reliability testing 8% Validation covers the required assembly process and customer-specified environmental or mechanical tests when applicable to the product. Reliability evidence is more extensive when the application requires high performance, including validation of crimping, sealing, retention, vibration, temperature, or fluid resistance as specified. Validation plan, test laboratory qualification, test reports, sample identification, failure analysis, corrective actions, and approval records. Confirm that test conditions match the product application and that samples are traceable to the released design and manufacturing process.
D. Delivery, Compliance, and Continuous Improvement
Nonconformance and corrective action 5% Defects are recorded, contained, reviewed, and corrected using a documented process with customer notification when required. The supplier demonstrates rapid containment, verified root-cause analysis, effectiveness checks, and trend monitoring for recurring or critical defects. Nonconformance reports, 8D or equivalent corrective-action reports, defect Pareto charts, containment records, and effectiveness reviews. Review recent cases from detection through closure and verify that corrective actions changed the relevant process control.
Packaging, labeling, and shipment protection 3% Harnesses are packed to prevent deformation, terminal damage, contamination, tangling, and loss of identification during normal transport. Packaging protects critical features during extended logistics, storage, and handling, with documented controls for moisture, electrostatic, or environmental risks when applicable. Packaging specification, shipping labels, packing-list records, drop or transport validation where required, and shipment inspection checklist. Inspect packed samples and confirm that part number, revision, quantity, lot information, and handling instructions are consistent with the order.
Capacity, lead time, and change management 4% The supplier has documented capacity planning, production scheduling, and notification procedures for material, process, tooling, or site changes. Capacity and change controls include documented contingency planning, qualification requirements, and customer approval before changes affecting critical performance. Capacity plan, bottleneck analysis, business-continuity plan, change-notification procedure, alternate-tool qualification, and delivery-performance records. Compare quoted capacity with actual equipment, staffing, test stations, tooling, and recent delivery performance for the intended program.
Overall supplier assessment 100% Approve when the supplier consistently meets the released design, applicable Class 2 requirements, inspection criteria, delivery obligations, and corrective-action expectations. Approve only when the supplier can demonstrate repeatable Class 3 controls, stronger traceability, validated processes, reliable testing, and effective control of high-consequence defects. Completed supplier audit, sample-build report, first-article report, capability evidence, quality agreement, and approved corrective-action plan. Use a weighted score together with mandatory-pass criteria for critical characteristics, electrical safety, traceability, and customer-specific requirements.
Buyer note: IPC/WHMA-A-620 class selection depends on the end-use application and customer requirements. Class 2 and Class 3 should be stated in the drawing, purchase order, quality agreement, or other controlling documentation. The standard does not replace product-specific engineering requirements, regulatory obligations, or customer acceptance criteria.

Production Capabilities: Crimping, Overmolding, and 100% Continuity Testing

China’s cable harness manufacturers serve global buyers with flexible production for automotive, industrial, medical, and consumer equipment applications. Experienced factories combine trained operators, controlled materials, and documented inspection procedures. Production quality begins with accurate drawings, suitable terminals, and verified wire specifications. Small details matter.

Crimping is a critical operation. Technicians adjust applicators according to terminal type, conductor size, and insulation thickness. They inspect crimp height, pull force, and bellmouth shape during production. Poor adjustment may create hidden resistance or weak mechanical strength. It happens. Reliable facilities use first-piece approval, calibrated tools, and regular sampling to reduce this risk. Clear work instructions also help different shifts maintain consistent results.

Overmolding adds protection where cables face moisture, vibration, abrasion, or repeated bending. Engineers select the resin and mold structure according to temperature and application demands. Trial runs should confirm fill quality, surface bonding, dimensions, and strain relief. A perfect appearance is not enough. Some defects develop inside the molded area. This is why process records and sample retention are valuable. 100% continuity testing then checks every finished harness for open circuits, short circuits, and incorrect connections. Test fixtures should match the approved wiring diagram and identify each unit. Test data provides traceability for buyers and supports corrective action when an issue appears. Manual inspection remains useful, although it cannot replace electrical testing.

Cable Harness Production Capability Benchmarks

The chart summarizes key production controls commonly required by global cable harness buyers: crimping quality verification, overmolding process inspection, and complete continuity testing. Continuity testing is shown at 100% coverage because every finished harness should be electrically verified before shipment.

Supplier Quality Proof: ISO 9001, IATF 16949, UL 486A-486B, and Traceability

For global buyers, cable harness quality begins with documented control, not attractive samples. ISO 9001 should shape daily procedures, from incoming wire inspection to final packing. Buyers should request current certificates, scope details, and audit dates. A certificate alone proves little. Process evidence matters more.

IATF 16949 indicates stronger automotive discipline, including risk analysis, process monitoring, and corrective action. At the crimping station, operators should record terminal type, crimp height, pull-force results, and tooling status. UL 486A-486B requirements support reliable wire-to-terminal connections. Samples should show secure crimps, correct strip lengths, and no exposed conductor damage. Small defects can create large field problems.

Traceability should follow every harness through production. A lot code can connect the wire reel, terminal batch, operator, machine, inspection record, and shipment date. Clear records make containment faster when an issue appears. Buyers should also review quarantine rules and rework approval methods. Some suppliers provide excellent documents but weak floor discipline. That gap deserves attention. Regular audits, retained samples, and realistic capability data reveal more than polished presentations. Supplier quality is never finished. It needs evidence, review, and occasional uncomfortable questions.

Global Buyer Comparison: MOQ, Lead Time, Pricing, Samples, and Export Compliance

For global buyers, comparing cable harness manufacturers requires more than a low unit price. Ask for MOQ by harness model, terminal type, and wire gauge. Some suppliers quote 100 pieces, yet custom tooling may require 500 units. A written MOQ schedule prevents costly surprises. Lead time should separate prototype, production, and inspection. In my sourcing reviews, a seven-day sample promise often excludes drawing approval. Ask for a dated production plan. Small details matter.

Request pricing at three volumes, such as 100, 1,000, and 10,000 assemblies. Confirm whether terminals, testing, packaging, tooling, and freight are included. A cheaper quote can become expensive after revisions. Samples should use production-intent materials, not substitute insulation or temporary connectors. Require dimensional reports, continuity-test records, and approval samples before mass production. Export compliance needs practical evidence: commercial invoices, packing lists, HS classification support, origin information, and documents required by the destination market. Verify restricted-substance declarations and traceability records. Requirements differ by country.

Tips: Send a controlled drawing with revision numbers, tolerances, photos, and test points. Ask for a sample timeline in writing. Compare landed cost, not factory price alone. Keep one approved sample for incoming inspection. I have seen delays caused by one missing connector specification. That mistake is avoidable, but not always obvious.