Choosing the right cable harness supplier can shape a product’s safety, consistency, and long-term cost. A polished sample is useful, but it never tells the whole story. Buyers should examine process control, material traceability, testing methods, and communication habits before signing an agreement.
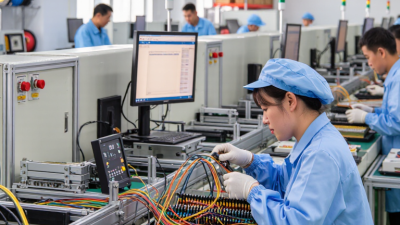
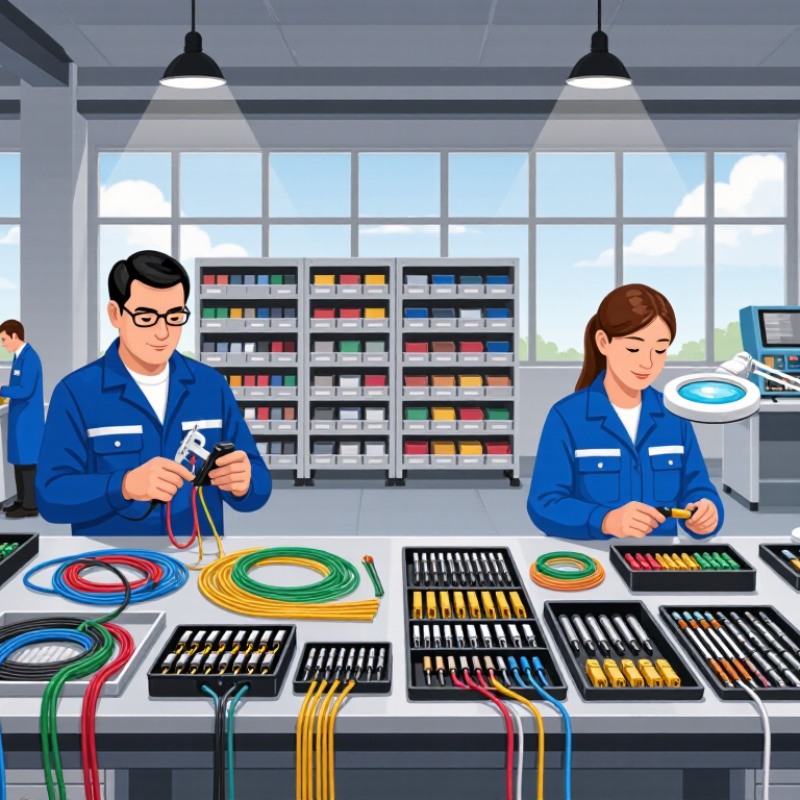
A capable supplier can explain wire specifications, connector compatibility, crimping standards, and inspection points in clear language. Ask how terminals are tested, how drawings are controlled, and how production changes are recorded. A factory visit may reveal practical details, such as labeled bins, calibrated tools, clean workstations, and operators checking pull-test results. These small signals often matter more than impressive brochures. Request samples from normal production, not specially prepared pieces. That comparison can expose weak workmanship.
Experience also matters, especially for complex assemblies with tight routing or demanding environments. However, experience alone is not proof of reliability. A long supplier list can hide poor follow-up. A modern facility can still miss a critical specification. That assumption can fail. Review customer references, quality records, delivery history, and corrective-action responses where possible. Confirm whether the supplier can support prototypes, volume production, and future design changes. Pricing deserves attention, but the lowest quote may bring higher rework costs later. Ask what the price includes, including testing, packaging, tooling, and engineering support.
The best decision balances technical ability, transparent communication, documented quality, and realistic capacity. It may take more time. That effort protects the finished product and the people who depend on it.
How to Choose the Right Cable Harness Supplier?
Start with a written harness specification. Define continuous current, peak current, operating voltage, cable length, bend radius, connector type, and IP rating. Current determines conductor size and terminal capacity. Voltage affects insulation thickness, spacing, and test requirements. Do not size conductors by current alone. Ambient temperature and bundled cables can reduce permissible load.
Measure length along the installed route, not across a flat drawing. I once treated length as a simple measurement. That was a mistake. A five-centimeter error can create tension at the connector. Specify connector keying, terminal plating, locking method, and mating cycles. Then request samples, crimp-force records, continuity results, and insulation-resistance data. IPC/WHMA-A-620 provides widely used workmanship criteria for cable and wire harness assemblies.
IP protection must match the real environment. IEC 60529 defines ratings such as IP54 and IP67, but enclosure performance depends on seals, cable exits, and assembly quality. Ask how the supplier validates water and dust resistance. The IEA’s Global EV Outlook 2024 reported nearly 14 million electric-car sales in 2023. This growth increases demand for high-voltage harnesses and stricter validation. Confirm voltage withstand tests, temperature cycling, vibration testing, and traceability. Cheap samples can look perfect. Production variation is harder to see. A reliable supplier should explain those gaps clearly.
Define harness requirements by current, voltage, length, connectors, and IP rating before requesting a quotation.
| Example harness profile | Current | Voltage | Length | Connectors | IP rating |
|---|---|---|---|---|---|
| Compact sensor harness | 3 A | 24 V | 1.5 m | 2 | IP67 |
| Vehicle auxiliary harness | 15 A | 48 V | 3 m | 4 | IP67 |
| Industrial power harness | 30 A | 600 V | 5 m | 6 | IP69K |
The chart expresses each requirement as a percentage of the reference envelope: 30 A, 600 V, 5 m, and 6 connectors. IP protection is shown separately as dust protection and water protection based on the two digits of the IP code. Confirm temperature range, insulation, bend radius, shielding, compliance requirements, and testing capability with the supplier.
Choosing a cable harness supplier starts with evidence, not polished photographs. Ask how the supplier applies IPC/WHMA-A-620 during production. This standard covers workmanship, crimping, soldering, routing, and connector assembly. Request inspection records, training details, and acceptance criteria for each harness type.
Look closely. During an audit, inspect crimp height, pull-test results, conductor strands, and terminal damage. Ask for continuity and insulation resistance test records. For safety-related assemblies, verify applicable UL certifications and confirm their scope covers your cable construction. A certificate alone may not cover every factory, material, or product family.
RoHS compliance needs more than a supplier declaration. Request material declarations, component information, and controls for restricted substances. Check whether updates are reviewed when terminals, insulation, or adhesives change. ISO 9001 certification can show a controlled quality system, but verify the certified site and scope. Review corrective-action records and traceability from incoming wire to final inspection.
Paperwork can look complete while production practices drift. That is easy to miss. I would also compare sample labels, batch records, and test data against an actual shipment. A capable supplier should explain failures without hiding them. Still, audits are only snapshots, and that limitation deserves attention. Ongoing inspections and clear change-notification rules provide stronger confidence.
| Compliance Area | Primary Purpose | What the Supplier Should Demonstrate | Recommended Evidence | How to Verify | Key Risk if Missing |
|---|---|---|---|---|---|
| IPC/WHMA-A-620 | Defines requirements and acceptance criteria for cable, wire, and harness assemblies. | Controlled workmanship standards, trained operators, documented inspection criteria, and consistent handling of soldered, crimped, terminated, and mechanically secured connections. | Applicable work instructions, operator training records, inspection checklists, process photographs, and sample first-article inspection reports. | Review the revision used, confirm that requirements are linked to drawings, and inspect representative samples against documented acceptance criteria. | Inconsistent workmanship, intermittent electrical faults, poor strain relief, terminal damage, or premature field failure. |
| UL Requirements | Addresses applicable safety requirements for certified wire, cable, components, or finished assemblies. | Use of appropriately rated materials and components, controlled substitutions, traceable certification information, and compliance with the applicable construction and usage requirements. | Applicable certification details, recognized component information, material specifications, construction documentation, and supplier change-control records. | Match the certification information to the exact cable, connector, insulation, temperature, voltage, and environmental requirements in the product specification. | Electrical safety concerns, unsuitable material ratings, failed regulatory review, or unauthorized component substitutions. |
| RoHS | Restricts specified hazardous substances in electrical and electronic products above defined maximum concentration values in homogeneous materials. | A documented restricted-substance control process covering wires, terminals, connectors, insulation, solder, plating, and purchased subassemblies. | Supplier declarations, material declarations, laboratory test reports where appropriate, bills of materials, and change-notification records. | Check the applicable market and directive version, confirm evidence covers all relevant materials, and verify that declarations are current and product-specific. | Non-compliant materials, restricted-market access, corrective-action costs, product recalls, or documentation delays. |
| ISO 9001 | Provides a framework for a quality management system based on controlled processes and continual improvement. | Defined quality objectives, document control, purchasing controls, production monitoring, nonconformity handling, corrective action, internal audits, and management review. | Valid certificate, stated certification scope, audit records, corrective-action examples, process maps, and quality performance data. | Confirm the certificate scope covers the relevant manufacturing activities, check validity dates, and assess how the system is applied on the production floor. | Uncontrolled processes, recurring defects, weak traceability, slow corrective action, and inconsistent delivery performance. |
| Engineering Capability | Ensures the supplier can interpret design data and prevent manufacturability problems before production. | Experience with drawings, cable schedules, bills of materials, tolerance requirements, termination specifications, and design-for-manufacturing reviews. | Design review records, manufacturability feedback, approved deviations, tooling plans, and first-article documentation. | Request a sample design review and ask the supplier to identify risks involving bend radius, routing, connector access, crimp height, and test points. | Design interpretation errors, assembly delays, repeated engineering changes, and avoidable tooling costs. |
| Electrical Testing | Confirms electrical continuity, isolation, polarity, and other specified performance characteristics. | Defined test coverage, calibrated equipment, controlled test programs, documented limits, and clear handling of failed units. | Continuity and hipot test records where specified, calibration certificates, test-program revision history, and failure-analysis reports. | Confirm test limits match the customer specification and verify that equipment calibration and test records are traceable to production lots. | Open circuits, shorts, incorrect pinouts, insulation breakdown, or undetected assembly defects. |
| Traceability and Change Control | Maintains control over materials, revisions, process changes, and affected production lots. | Lot or batch identification, approved supplier lists, revision-controlled drawings, documented substitutions, and formal customer notification procedures. | Material receiving records, traveler documents, revision history, deviation approvals, and change-notification examples. | Trace one finished harness backward to materials, operators, equipment, inspection results, and the applicable drawing revision. | Unclear containment, mixed revisions, difficult root-cause analysis, and costly field corrections. |
| Final Supplier Qualification | Combines compliance, quality, capacity, cost, and delivery capability into a documented sourcing decision. | Transparent responses, realistic lead times, stable capacity, clear escalation contacts, and willingness to support audits and corrective actions. | Completed supplier questionnaire, audit scorecard, sample evaluation, capability study, pilot-run results, and corrective-action plan. | Use a weighted scorecard and require documented closure of critical gaps before approving serial production. | Unexpected quality costs, missed delivery commitments, compliance gaps, and limited recovery options. |
Choosing a cable harness supplier requires more than checking a glossy capability sheet. Compare the details that affect your assembly line: AWG range, tolerance, MOQ, and lead time. A supplier may list 30–10 AWG, yet struggle with your thin 32 AWG signal wire. Ask for samples across the actual range. Inspect crimp height, insulation position, and conductor pull strength.
Tolerance shows whether production stays stable or shifts between batches. Request dimensional limits for wire length, terminal position, stripping, and connector fit. A reliable supplier should explain its gauges, inspection frequency, and measurement records. Do not accept “tight tolerance” without numbers. For example, a 1 mm variation may be harmless in a loose enclosure but costly beside a moving actuator. This is where engineering evidence matters.
MOQ and lead time reveal commercial flexibility. A low MOQ helps prototype teams avoid storing thousands of unused harnesses. However, an unusually low MOQ may hide setup charges or limited material availability. Confirm lead times for samples, first production, and repeat orders. Ask what happens when terminals, drawings, or materials change. In my experience, suppliers sometimes promise quickly before reviewing tooling and test requirements. That deserves a second check. Compare written commitments, not confident phone calls. A small pilot order can expose unclear tolerances, packaging damage, or weak communication before volume production begins.
Choosing a cable harness supplier should begin with evidence, not polished samples. A reliable quality system makes each harness traceable from incoming wire to final shipment. Ask for lot numbers, operator IDs, crimp-tool settings, inspection records, and rework history. These details should connect to the finished harness through a controlled digital or paper trail. Small details matter. If a terminal later shows abnormal resistance, the supplier should locate the affected lot quickly. That response reveals more than a certificate on the wall.
100% continuity testing is another practical checkpoint. Every assembled circuit should be tested for opens, shorts, and incorrect connections before packing. Ask how test fixtures are validated and how failed units are isolated. A screen showing “pass” is not enough. Test records should identify the harness, date, program version, and operator. Yet testing has limits. A continuity check may not detect weak crimps or damaged insulation. The supplier needs complementary controls, such as pull-force checks, visual standards, and periodic dimensional audits.
PPM data helps measure consistency over time. Request defect rates by month, product family, and failure type, rather than one impressive annual number. Review trends after tooling changes, material substitutions, or production transfers. Low PPM is useful, but definitions matter; hidden rework can make performance look better than it is. A thoughtful supplier explains misses openly and tracks corrective actions to closure. That honesty may feel uncomfortable. It is often more valuable than perfection claimed too quickly.
Choosing a cable harness supplier requires more than comparing unit prices. Proven PPAP capability should be visible in sample records, dimensional reports, material certificates, and traceability logs. The AIAG PPAP framework emphasizes documented evidence that production processes can meet customer requirements consistently.
Ask to review a redacted submission, not just a presentation.
IATF 16949 certification adds process discipline across risk management, supplier control, measurement, and corrective action. The ISO Survey 2023 reported IATF 16949 certificates across more than 160 economies, showing its broad automotive relevance.
However, certification alone is not proof of strong execution. Audit the supplier’s PFMEA, control plan, special-process controls, and change-notification history. Small gaps matter.
Lifecycle support should cover engineering changes, tooling maintenance, replacement materials, field failures, and end-of-life planning. The Automotive Industry Action Group identifies structured problem-solving and customer-specific requirements as important quality practices.
In practice, request response-time targets and recent 8D examples. Check whether production data can trace a harness to its lot, operator, test result, and shipment date.
I have seen suppliers pass an initial audit but struggle after volume increases. That weakness deserves honest attention. A capable partner supports the harness from first article approval through years of service, with clear evidence at every stage.